Current condition
Record a sample identifier, assembly variant, joint feature, reference decision and the person or team responsible for that decision. Note sample condition and any uncertainty or disagreement before using it as a reference.
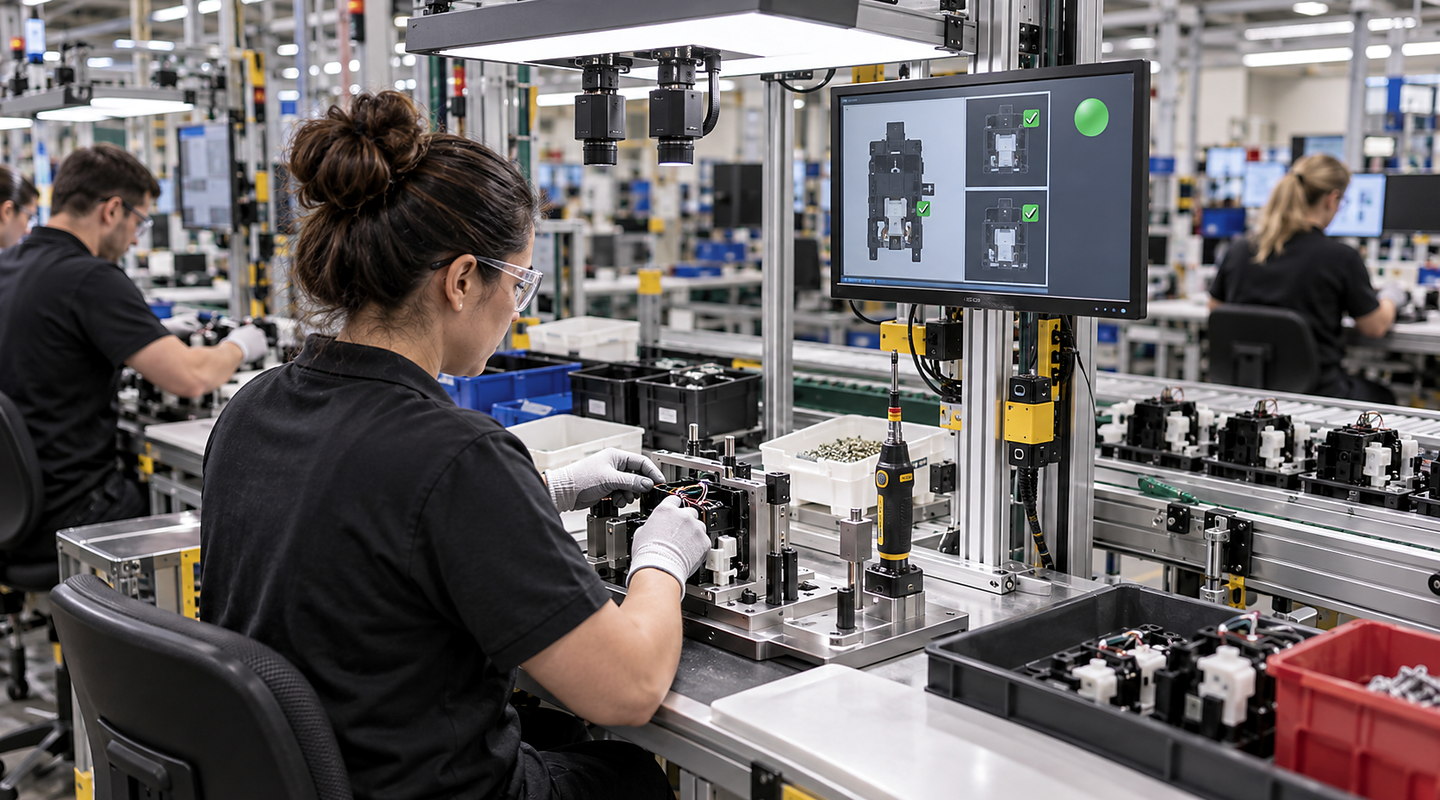
What decisions about good, bad and marginal sample range materially change the system concept for solder joint inspection?
Build the solder-joint sample set around the visible features and decisions approved by the electronics quality team. Label accepted, rejected and marginal examples, include normal variation and keep every sample linked to its reference decision and assembly variant.
Use the set to assess viewing access, lighting, presentation and timing, while recording features that remain hidden or unclear. The challenge-test guide separates sample coverage from the final acceptance decision.
Plan solder joint inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Use this guide to resolve good, bad and marginal sample range before it limits the final system.
Discuss your application

Record a sample identifier, assembly variant, joint feature, reference decision and the person or team responsible for that decision. Note sample condition and any uncertainty or disagreement before using it as a reference.
Include accepted appearance variation as well as the rejected and marginal cases within the proposed duty. Cover representative variants, presentation and component shadows; do not rely only on obvious defects or hand-selected ideal assemblies.
Record whether each sample's relevant feature is visible under the tested setup and whether the recorded result agrees with its reference decision. Preserve obscured, inconclusive and untested cases as limitations rather than counting them as demonstrated coverage.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for visible defect or measurement definition for visible solder-joint inspection. That lets us compare options against your real production rather than one nominal value.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for part presentation and production speed. That lets us compare options against your real production rather than one nominal value.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for optics, lighting and environmental conditions. That lets us compare options against your real production rather than one nominal value.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.
For Good, Bad and Marginal Sample Range: Optics and lighting selection, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.